Measurement fundamentalsReading time 13 min
Resolution Is Not Measurement Capability
A display that reads 0.001 mm does not prove that a 0.01 mm tolerance can be judged reliably. Separate resolution, repeatability and uncertainty before choosing a gauge or accepting a result.
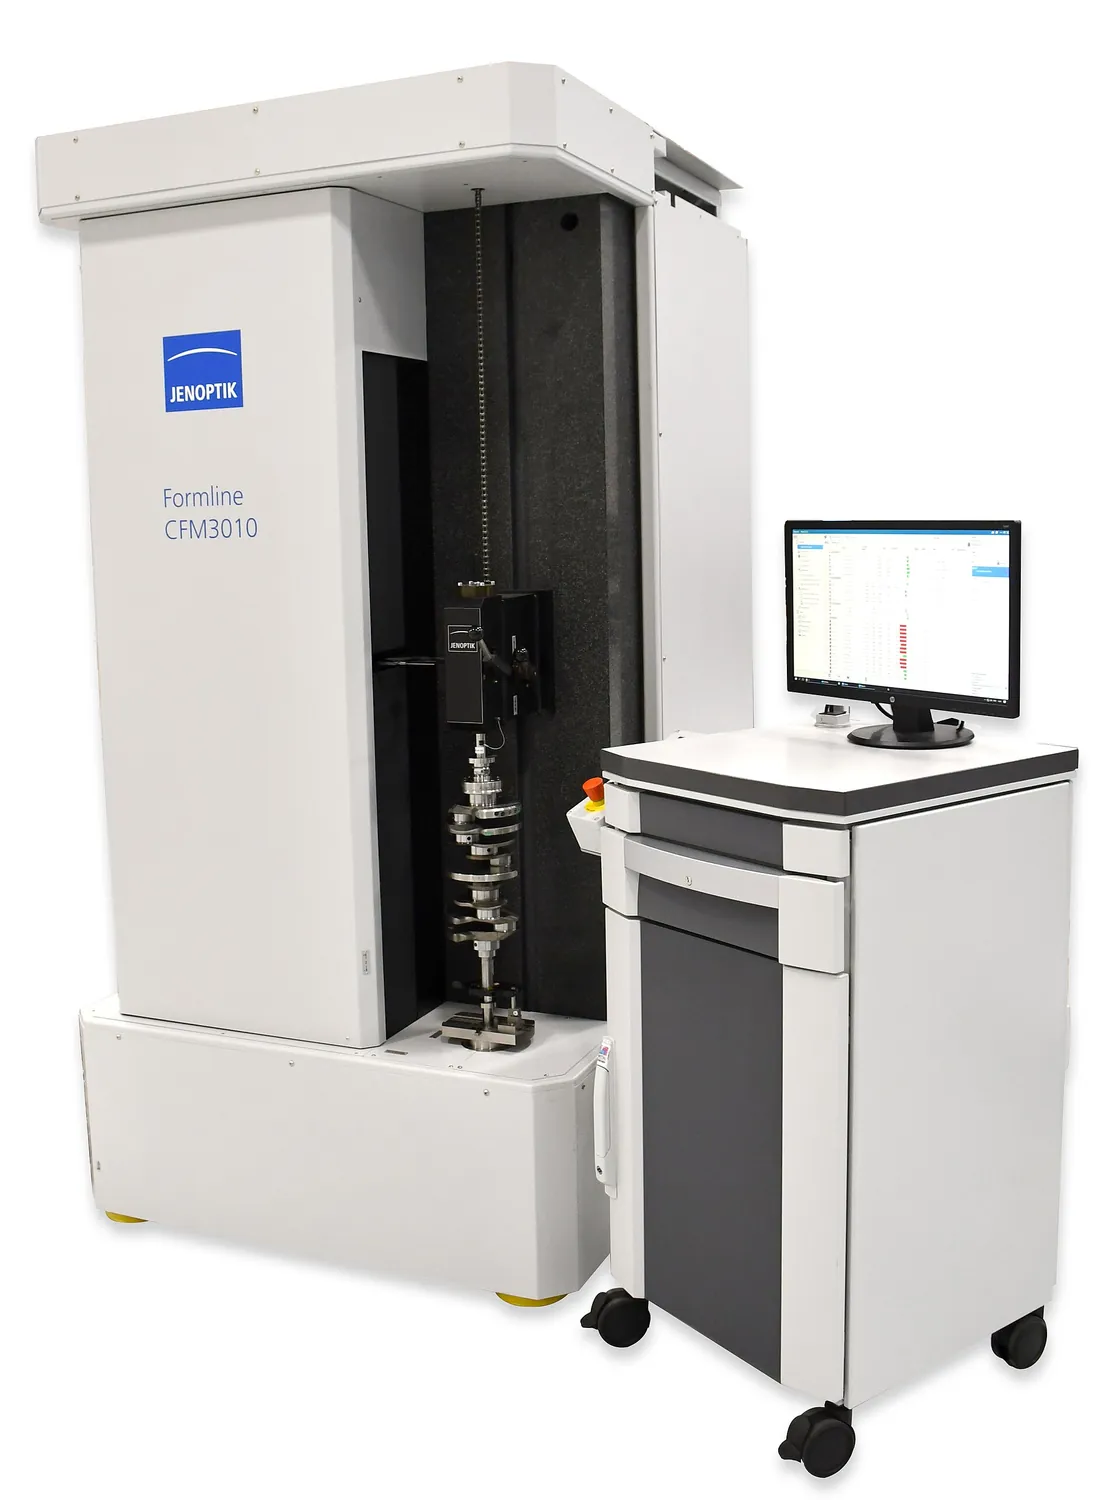 Wikimedia Commons・Example of a Cylindrical Coordinate Measuring Machine・CC BY-SA 4.0
01Four measurement terms
| Term | Definition | In plain language |
|---|---|---|
| Resolution | The smallest increment the instrument can display | How much one step on the screen is worth |
| Accuracy | How close a reading is to the true value | Is it systematically off |
| Precision / repeatability | The spread of repeated readings under the same conditions | Will ten readings agree |
| Uncertainty | A quantified statement of the interval you can trust | How far can you believe this number |
A digital caliper may display 0.01 mm increments, yet its result also depends on measuring force, alignment, temperature and the operator. Those effects are not visible on the screen. Before accepting a close-to-limit result, compare the total measurement uncertainty with the tolerance.
The Abbe principle
Abbe's principle favors a measuring scale aligned with the dimension being checked. Caliper jaws sit away from their scale, so jaw tilt can add error. A micrometer's geometry reduces that particular effect, though its suitability still depends on the feature and measurement range.
02What GR&R measures
Gauge R&R separates variation from repeated readings by one operator and variation between operators. Use it to see whether the measurement method can distinguish real part differences from measurement noise.
| %GR&R | Verdict | Action |
|---|---|---|
| < 10% | Acceptable | Fit for process control |
| 10% ~ 30% | Conditionally acceptable | Decide on the importance of the application and the cost of improvement |
| > 30% | Not acceptable | The measurement system must be improved |
03Matching gauge to feature
| Instrument | Typical resolution | Typical uncertainty | Typical use |
|---|---|---|---|
| Vernier caliper | 0.02 / 0.01 mm | ±0.03 mm | Quick checks on the floor, coarse tolerances |
| External micrometer | 0.001 mm | ±0.004 mm | Outside diameters, plate thickness, IT7 and looser |
| Lever dial indicator | 0.001 mm | ±0.003 mm (comparative) | Runout, parallelism, setting up |
| Gauge blocks (grade 0) | — | ±0.1 μm class | Calibration reference |
| Optical comparator / vision system | 0.001 mm | ±0.002 mm | Two-dimensional profiles, many features at once |
| Coordinate measuring machine | 0.0001 mm | MPE varies by model | Three-dimensional features, geometric tolerances |
| Roundness tester | 0.01 μm | Sub-micron | Roundness, cylindricity |
Contact and non-contact
- Contact methods are unaffected by surface colour or gloss and have mature traceability, but every point has to be touched, complex profiles are slow, and measuring force deflects thin or soft parts.
- Vision systems capture hundreds of dimensions at once and suit sheet and stamped parts, but they cannot see height, and edge detection depends on surface condition and lighting.
- Laser and confocal reach into deep holes and cope with high-contrast surfaces, but distort on steep slopes and transparent materials.
04Temperature effects
Dimensional metrology commonly uses 20 °C as a reference temperature. Materials expand at different rates, so a long aluminum part can shift noticeably between a warm shop floor and a controlled room. Record temperature when the tolerance makes it relevant.
| Materials | Expansion coefficient (μm/m·K) | Change on a 500 mm part, 8 °C rise |
|---|---|---|
| Carbon steel | 11.7 | 47 μm |
| Stainless 304 | 17.3 | 69 μm |
| Aluminium alloys | 23.1 | 92 μm |
| Brass | 19.0 | 76 μm |
| Cast iron | 10.5 | 42 μm |
05Choosing a method
- Start with the feature. Two-dimensional profile or three-dimensional form? Are there geometric tolerances that need datums?
- Then look at the tolerance band. Aim for measurement variation below one tenth of the band.
- Then throughput. Sampling or 100% inspection? How many a day? What is the takt?
- Finally traceability. Does the customer want an inspection report, or a calibration certificate?
Match the method to the characteristic and production flow. A CMM suits complex three-dimensional geometry; vision may support high-volume two-dimensional checks; calipers and micrometers remain useful when their uncertainty is small enough for the tolerance.