Manufacturing processesReading time 12 min
Sheet-Metal Flat Patterns: Account for the Bend
The flat blank is not the sum of the finished side lengths. Bend radius, thickness and K-factor determine the bend allowance. Get that calculation wrong and the part is short before forming begins.
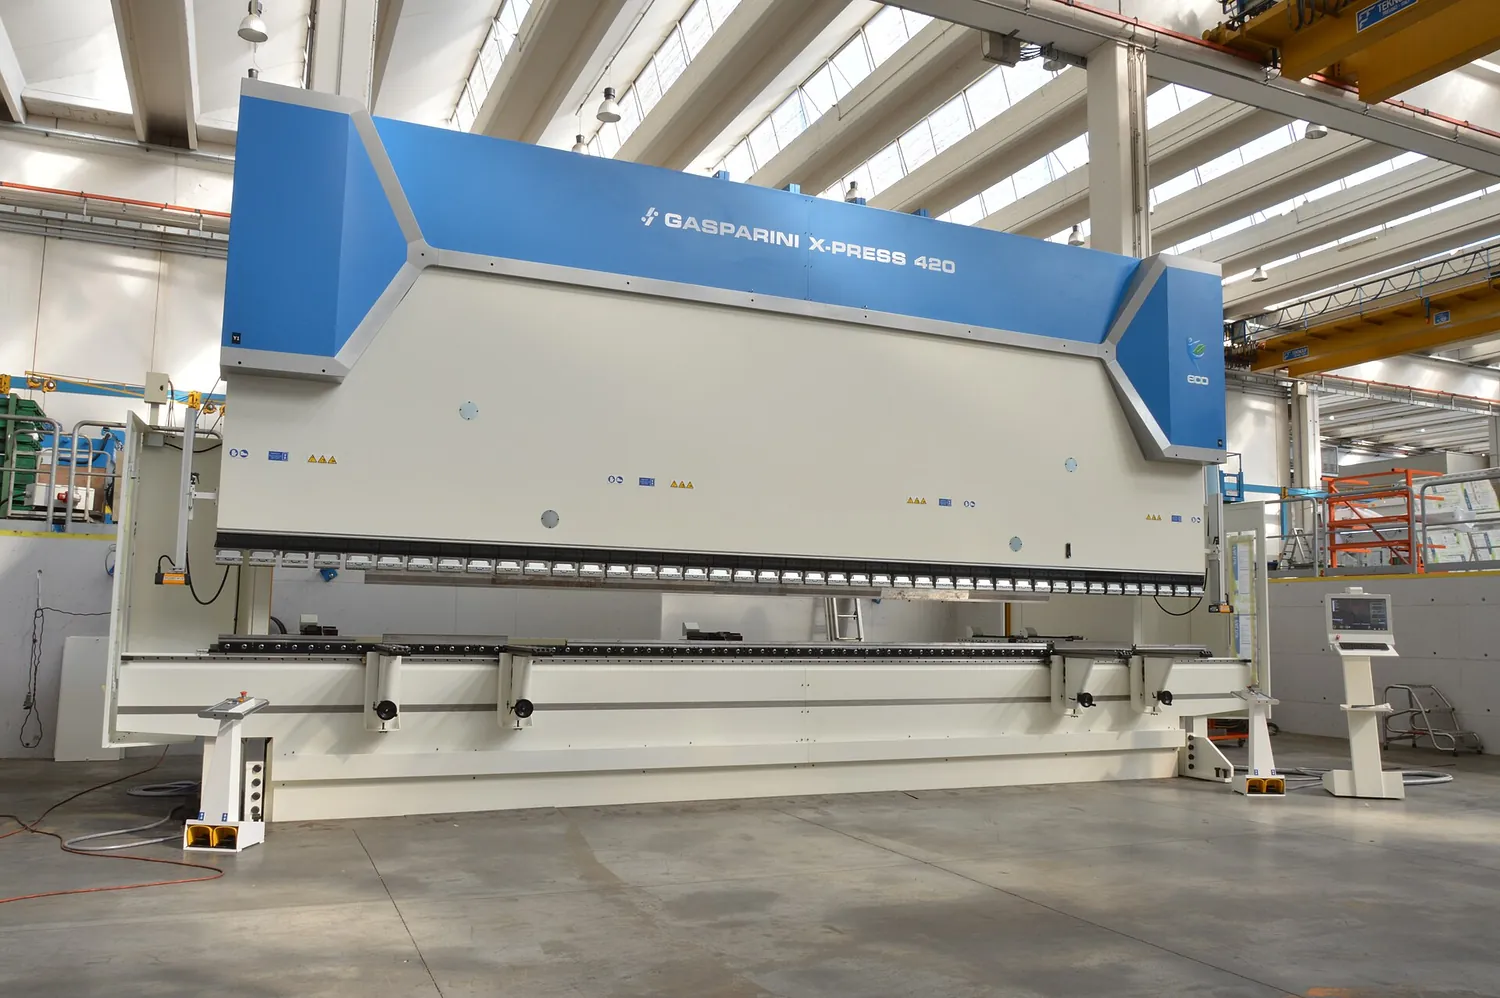 Wikimedia Commons・High-tonnage press brake・CC BY-SA 4.0
01Calculating the flat length
During bending, the outside of the sheet stretches and the inside compresses. Between them lies a neutral layer whose length is used to calculate the flat pattern. It is not necessarily at mid-thickness, so adding the finished leg lengths will not give the correct blank size.
| Term | Symbol | Meaning |
|---|---|---|
| Thickness | T | Material thickness |
| Inside radius | R | Radius of the corner on the inside of the bend |
| Bend angle | A | How many degrees it bent through (not the included angle) |
| K factor | K | Neutral axis position ÷ thickness, between 0 and 0.5 |
| Bend allowance | BA | Arc length of the neutral axis through the bend |
| Bend deduction | BD | What to subtract after adding the two outside lengths |
Two ways to calculate
- Bend allowance method. Flat length = the two flat lengths + BA, where BA = A × (π/180) × (R + K×T).
- Bend deduction method. Flat length = the two outside lengths − BD. Shops use deduction more often, because outside dimensions can be measured directly.
02Choosing the inside radius
In air bending, the inside radius depends strongly on die opening, material and tooling—not just the radius written on the print. Check whether the available tooling can make the specified radius before releasing the blank.
| Materials | Minimum inside radius (× thickness) | What it asks |
|---|---|---|
| Soft aluminium 1050 / 3003 | 0.5 T ~ 1 T | Very ductile |
| Aluminium 5052 | 1 T ~ 2 T | The usual sheet-metal aluminium |
| Aluminium 6061-T6 | 2 T ~ 4 T | Hard, cracks easily |
| Mild steel SPCC | 0.5 T ~ 1 T | The easiest to bend |
| Stainless SUS304 | 1 T ~ 2 T | Large springback |
| High-strength steel | 2 T and above | Depends on grade |
Springback
Metal springs back after the press releases. The amount depends on material strength, thickness, radius and process, so trial bends or a proven bend table are more reliable than a universal overbend angle.
03Spacing holes and bends
| Item | Suggested minimum | What happens if you ignore it |
|---|---|---|
| Hole to bend line | 2.5 T + R | The hole is drawn into an oval |
| Shortest bent flange | 4 T including the radius | Cannot be gripped or formed |
| Between two bends | 6 T | Tooling interference |
| Notch width | 1.5 T | Tearing |
| Slot depth | 5 T | Edge distortion |
Also check where a bend terminates and in what order bends can be made. Relief cuts prevent tearing at the end of a bend; a feasible sequence prevents a formed flange from colliding with the tool on the next operation.
04What the drawing should show
- Thickness and material grade, including surface condition such as SPCC-SD.
- Flat pattern or flat length, if the customer does not supply it, you must calculate it, and the K factor has to match your own machine.
- Bend lines and direction (up or down), preferably with angle and inside radius.
- Datum for hole positions, which face, after bending, they are measured from.
- Deburring and surface treatment requirements, and whether dimensions are before or after treatment.